Kitchen countertops and vanity tops on a CNC bridge saw
A 5-axis CNC bridge saw cuts the full kitchen from a DXF: straight cuts, miters, cooktop and sink cutouts with an electrospindle, and drainboard grooves. Most of the time it saves is handling time between cuts, not cutting speed.
From template to DXF
The job starts at the customer’s cabinets. A digital templater (laser or photogrammetry) measures the walls, cabinet runs, appliance positions and sink centerline, and the drawing is exported as DXF. The DXF goes into the saw’s CAM or an offline programming station, where the fabricator adds edge types, overhangs, cutouts and seam positions.
Check the design rules of the material before nesting. They differ between products:
| Rule | Engineered quartz (Compac) | Sintered / porcelain (Laminam 12+/20+) | Dekton Lite (Cosentino) |
|---|---|---|---|
| Inside corner of L or U top | min. R10 mm (3/8 in) | min. R5 mm | min. R5 mm, mandatory |
| Sink cutout corner | min. R20 mm | min. R5 mm | R20 mm recommended |
| Cutout to slab edge | 50 mm (2 in) from corners for accessory holes | see guide | min. 50 mm to edge, 150 mm to joints |
| Drainboard grooves | max. 4 mm deep, min. 6 mm apart | see guide | not allowed |
The Staron Locelain manual asks for at least 50 mm between a cutout and the edge and at least 50 mm between a faucet hole and the cutout. Where the manufacturer and the sink maker give different radii, use the larger one.
Slab photo layout, nesting and vein matching
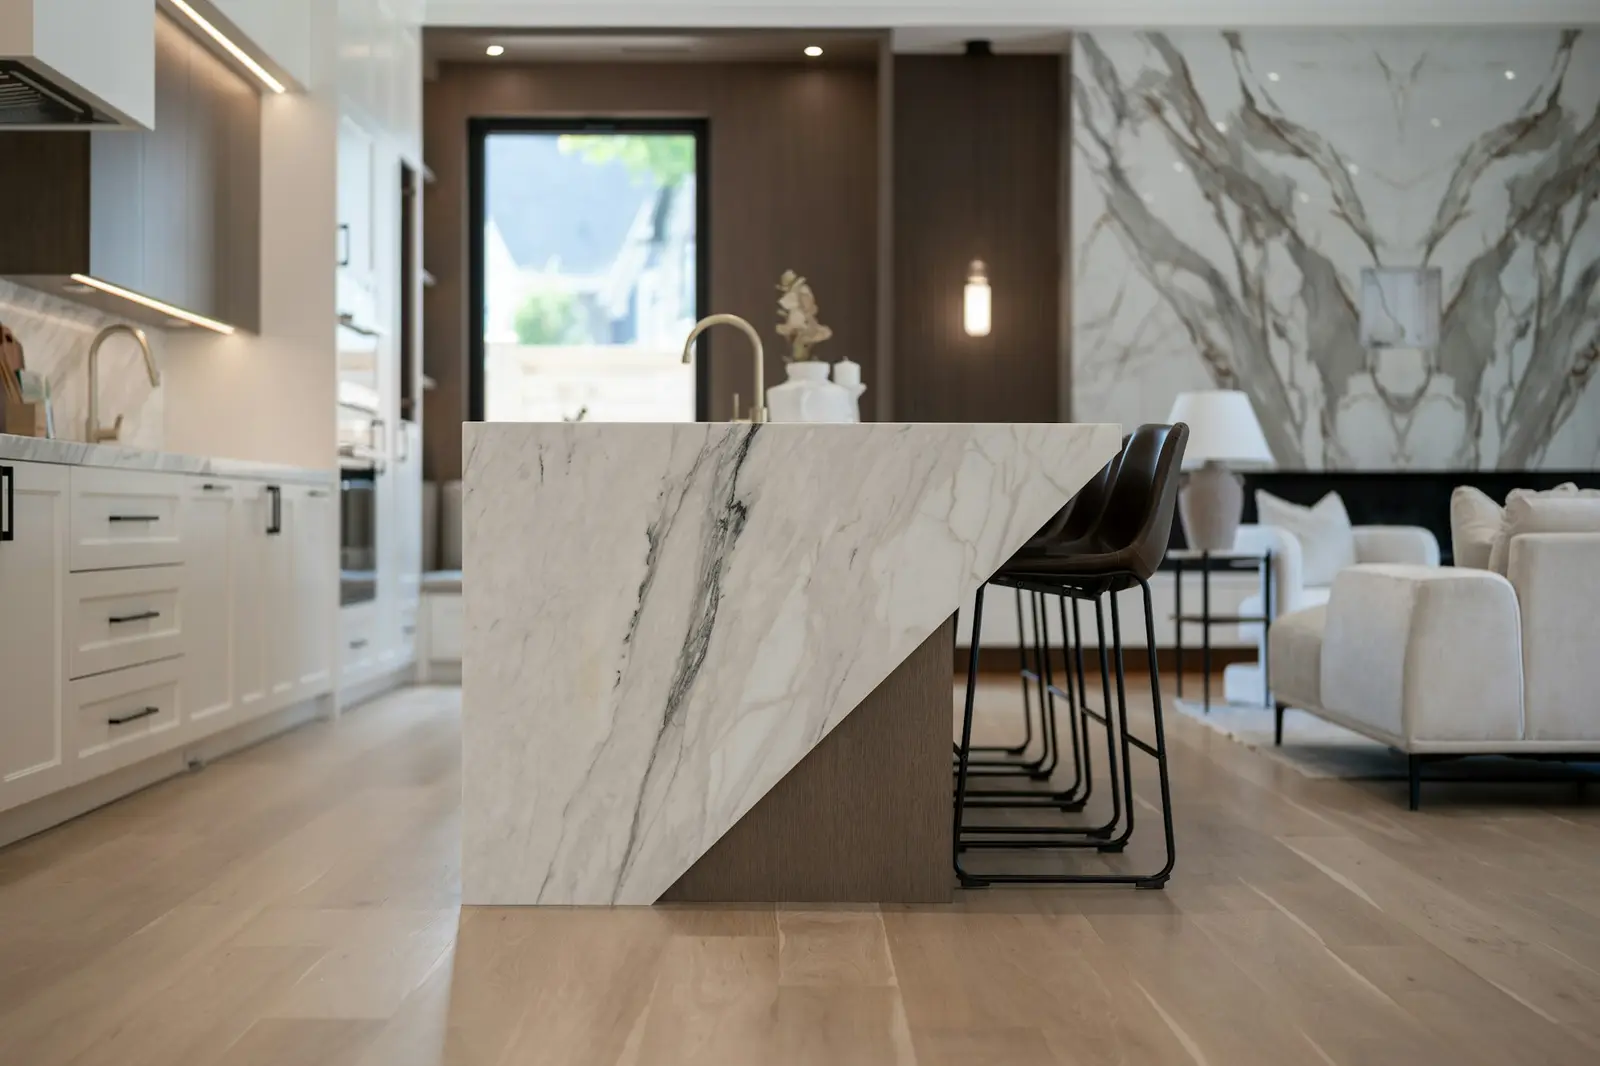
With a digital camera over the worktable, the saw photographs the loaded slab and the operator places the pieces on the real image. This is where vein matching happens: the island top and its waterfall end are placed next to each other so the veins run over the miter, and seams on an L-shaped run are placed where the pattern can continue across the joint.
Nesting is a compromise between yield and appearance. For plain quartz, pack the pieces tightly and keep offcuts large enough for vanity tops and backsplash strips. For a bookmatched marble or a veined porcelain, the layout follows the pattern and yield drops. Decide this with the customer before cutting, not at the saw.
For porcelain and sintered slabs, the layout also needs space for perimeter trimming. Laminam asks fabricators to square untrimmed “full size” slab edges first. Staron recommends removing 20–30 mm around the edges before any other cut, to release internal stress.
Cutting sequence
A typical sequence on a 5-axis CNC bridge saw:
- Trim and straight cuts. Rip the slab into the main runs. Do not plunge in the middle of a porcelain slab; start from outside the slab. Reduce feed at entry and exit. Laminam asks for 50% feed over at least one blade diameter. Staron gives 50% over 15–20 cm.
- Miters. Tilt the A-axis to 45° for apron (drop-edge) strips and waterfall ends. Cut the apron strip from the same slab area as the top it sits under so the vein continues. See mitered edges for accuracy and chipping control.
- Cooktop cutout. Drop-in cooktops do not need a polished cutout edge. The blade makes the straight cuts; a core bit on the electrospindle drills the corner radii first so the blade never overcuts into the corner. Laminam describes the same logic for disc cutting: drill the corners, then cut straight between the holes.
- Sink cutout. An undermount sink needs a polished inside edge, which means contouring and polishing with the electrospindle and tool changer. This is a long cycle. Many shops leave it to a separate CNC work center and keep the saw cutting.
- Drainboard grooves. Milled with a grinding wheel or cut with the blade at shallow depth and inclined Z. Respect the material limit (4 mm for Compac quartz; none allowed on Dekton Lite).
- Rodding. Grooves cut in the underside along the front and back rails of the sink cutout, where the top is narrow. A fiberglass rod (for example 1/8 × 3/8 in section) is bonded in with countertop adhesive. Rodding is common on natural stone and narrow quartz sections; check the slab manufacturer before rodding sintered material, since Laminam relies on bonded slats under the cutout instead.
Piece handling with the vacuum manipulator
After a cut the pieces sit tight against each other. The next cut often needs them apart, and on a manual workflow the operator stops the saw to slide or lift them. A vacuum manipulator on the head picks a cut piece, moves it clear, or rotates it so the next edge faces the blade. On a kitchen with ten to twenty pieces, these moves add up to more time than the cuts themselves.
The 5-axis head saves handling in three places:
- Miters are cut on the same setup as straight cuts. No second machine, no re-measuring.
- Cutouts and drainboard grooves are done without moving the top to another station, if the shop chooses that.
- Pieces are rotated by the manipulator rather than by two people, which matters for 30 mm granite tops and for long sintered pieces that crack if they twist.
What drives kitchens per shift
We do not publish a kitchens-per-shift figure, because it depends on the job mix more than on the machine. The main drivers:
- Material. Laminam’s recommended feed for straight cuts in 20 mm sintered slab is 800–1,000 mm/min. Granite and quartz run faster. A porcelain kitchen with mitered aprons takes much longer than a quartz kitchen with eased edges.
- Number of miters and cutouts. Inclined cuts run at roughly half the straight-cut feed in Laminam’s table.
- Where cutouts and polishing happen. Milling a polished undermount cutout on the saw can tie it up longer than all the sawing in the kitchen.
- Programming offline. If the next job is programmed while the saw cuts, the saw does not wait.
- Slab loading. Loading time with a forklift or vacuum lifter is fixed per slab and does not shrink with a faster saw.
- Blade changes. A dedicated miter blade or porcelain blade means a change when the material changes.
Tooling
- Saw blades: granite, quartz and porcelain blades are different specifications. Porcelain usually needs a blade made for it, with a reinforced or silent core for inclined cuts. Laminam recommends a smaller blade diameter or flange and counterflange for inclined cuts.
- Core bits for corner radii and faucet holes.
- Finger bits and grinding wheels for contouring and drainboard grooves on the electrospindle.
- Polishing tools if undermount cutouts are finished on the saw.
Countertop, worktop, benchtop
The product is the same; the word changes with the market. “Countertop” is US usage, “worktop” is UK and much of Europe, and “benchtop” is Australian. Cosentino’s manual uses “worktop”; Compac’s US manual uses “countertop”. If you sell into several markets, put the local term in quotes and drawings.
Next step
Send us a typical kitchen drawing and your material mix through request a configuration, and we will propose a saw setup for it. The full specification table is on the 5-axis CNC bridge saw page.
Sources
- Laminam: Technical guide for furnishing & design, 12+ and 20+ (06.2021)
- Compac: Technical manual of design and installation of countertops, Quartz and Obsidiana (2022)
- Cosentino: Dekton Lite worktop manufacturing and fitting manual
- Lotte Chemical (Staron): Locelain technical manual, fabrication for countertop LN-303-2019
- Chemical Concepts: Economy fiberglass countertop rodding